Advanced Chemical Liquid Stirring 100L Electric Heating Vacuum Reactor & Syrup Manufacturing Vessel Pakistan
Quick answer: Morgan Chemicals supplies Advanced Chemical Liquid Stirring 100L Electric Heating Vacuum Reactor & Syrup Manufacturing Vessel Pakistan across Pakistan as part of its Syrup Manufacturing Machines range, with quotations available via info@morgan.pk.
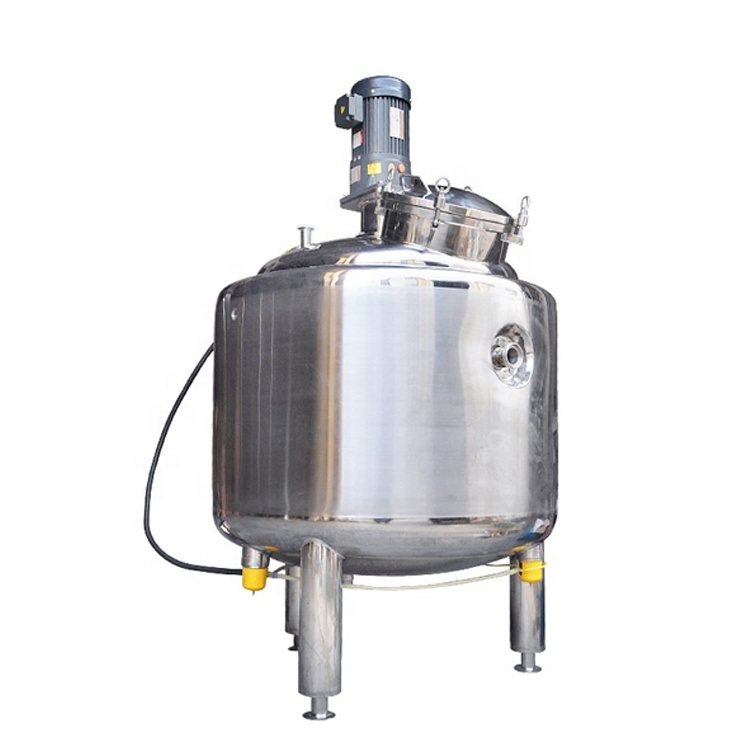
In the demanding fields of chemical processing, pharmaceutical formulation, and commercial food production, managing thermal reactions and fluid dynamics is a highly critical operational requirement. Handling viscous fluids, suspended solids, and complex liquid mixtures requires highly specialized equipment capable of maintaining precise environmental controls. The Chemical Liquid Stirring 100L Electric Heating Vacuum Reactor is engineered to execute precise mixing, rapid thermal transfer, and controlled pressure reactions without introducing environmental pollution or risking material degradation.
Furthermore, this versatile equipment functions exceptionally well as a heavy-duty syrup manufacturing vessel, accelerating the dissolution of sugars and thick liquid additives in the food and beverage industry. For manufacturing facilities seeking to upgrade their liquid processing lines, finding a reliable equipment partner is a major operational priority. Supplied and expertly integrated by Morgan Technologies, this robust stainless steel reactor delivers exceptional corrosion resistance and high-temperature stability, ensuring maximum operational efficiency and strict compliance with global manufacturing standards in Pakistan.
Engineered for Precision: Heating, Vacuum, and Stirring Mechanisms
Standard mixing tanks often fail when processing highly viscous materials or conducting temperature-sensitive chemical reactions. This advanced reactor overcomes these limitations through a highly engineered combination of thermal control, vacuum technology, and variable-shear agitation.
Advanced Electric Heating and Thermal Control
-
Rapid Thermal Transfer: The reactor utilizes an advanced electric heating system integrated directly into the jacket. This allows for rapid heating and precise temperature maintenance, which is essential for sensitive chemical synthesis, biological fermentation, and syrup melting.
-
Multi-Layer Jacketed Design: The vessel can be configured with a single, double, or triple jacket. This cellular cooling and heating jacket structure effectively improves the heating and cooling speed according to specific process requirements.
-
Premium Insulation: To maximize energy efficiency and protect facility operators from extreme surface temperatures, the tank is wrapped in high-density polyurethane foam or rock wool insulation. This prevents critical heat loss during extended operating cycles.
High-Performance Stirring and Emulsification
-
Customizable Agitator Profiles: To handle varying liquid viscosities and suspended solids, the reactor supports multiple mixer types. Options include impeller-type, anchor-type with Teflon scrapers, turbine-type, magnetic mixers, and high-shear dispersing units.
-
Variable Speed Control: Powered by robust motors (ranging from 1.5 kW to 55 kW depending on the scale), the agitator speed is fully adjustable. Utilizing a Variable Frequency Drive (VFD), operators can safely manage the inverted speed from 0 up to high-RPM ranges to prevent air bubble formation during liquid formulation.
-
Suspended Solids Management: The powerful torque ensures that liquids with suspended solids and highly viscous fluids are blended uniformly without stalling the motor or causing uneven concentration gradients inside the vessel.
Vacuum and Pressure Operations
-
Degassing and Evaporation: The reactor is designed to sustain highly stable vacuum conditions. This allows for the rapid degassing of thick chemical liquids and syrups, low-temperature evaporation of sensitive solvents, and the secure handling of volatile compounds in a completely closed loop.
Premium Structural and Sanitary Design
When investing in a commercial-grade chemical reactor or food-grade processing tank, the physical architecture must facilitate rapid sanitation, operational safety, and long-term mechanical durability.
-
High-Grade Stainless Steel: The entire internal reaction vessel and all product-contact components are constructed from premium SUS 316L stainless steel (typically 3mm thick). The outer jackets and non-contact cladding utilize durable SUS 304 stainless steel (2mm thick).
-
Optimized Bottom Design: Depending on the application, the vessel is engineered with a standard dished end or a 60-degree conical bottom (customizable to 70 or 90 degrees). This specialized conical geometry vastly improves yeast breeding, fermentation efficiency, and the final discharge of heavy syrups.
-
Comprehensive Certifications: The equipment is manufactured to meet the highest international safety and quality standards, including ASME, CE, GMP, UL, ATEX (for explosion-proof requirements), and ISO 9001.
-
Hygienic Integrations: The tank features all-closed dust holes, a sanitary inspection manhole, sample extraction ports, and internal CIP (Clean-In-Place) cleaning heads, allowing the vessel to be fully sanitized and validated without manual disassembly.
Diverse Industrial Applications
Thanks to its modular design and robust thermal capabilities, this electric heating vacuum reactor acts as a versatile asset across multiple highly regulated sectors:
-
Chemical & Petrochemical Industry: Essential for executing high-temperature vulcanization, nitrification, and polymerization. It is used heavily in the production of commercial resins, agricultural pesticides, industrial pigments, and advanced rubber processing.
-
Pharmaceuticals & Cosmetics: Utilized for blending highly viscous medicinal ointments, compounding active pharmaceutical ingredients (APIs), and producing homogeneous cosmetic lotions under strict vacuum conditions to eliminate oxidative air pockets.
-
Food, Beverage & Brewery: Functions as a highly efficient blending mixer and syrup manufacturing vessel. It is ideal for the hygienic blending of thick food additives, preparing clear sugar syrups, dairy processing, and operating as a stainless steel fermenter for brewing applications.
Technical Specifications
Morgan Technologies provides this reactor in a highly scalable format, starting from the agile 100L model up to massive industrial vessels, ensuring an exact match for your facility's output requirements.
| Specification | Details |
| Working Capacity | 100 Liters (Scalable from 50L up to 30,000L / 100-200 Gallons) |
| Heating Method | Electric Heating (Steam heating optional) |
| Material Construction | Contact Parts: SUS 316L (3mm) / Outer Jacket: SUS 304 (2mm) |
| Mixer Types | Anchor with scrapers, Impeller, Turbine, High-shear |
| Motor Power | 0.75 kW to 55 kW (Depending on capacity and fluid viscosity) |
| Operating Speed | 0 - 63 rpm (Adjustable via inverter), higher speeds for dispersion |
| Jacket Configuration | Cellular cooling/heating jacket with Polyurethane foam insulation |
| Voltage | 110V to 600V / 380V, 50Hz, 3-Phase (Customizable) |
| Vessel Bottom Design | 60° / 70° / 90° Conical Bottom or Standard Dished End |
| Safety & Control | Thermostatic settings, Electric-control box, Optional Explosion-proof device |
Partnering with an Expert Supplier in Pakistan
Procuring a highly complex chemical reactor or commercial syrup vessel requires an engineering partner capable of ensuring continuous, safe, and high-volume operational success. As a leading supplier of advanced industrial mixing equipment, Morgan Technologies delivers complete, end-to-end integration for your processing facility.
When you select Morgan Technologies, we manage the entire project lifecycle. Our specialized engineering teams handle the complete physical installation and commissioning, expertly connecting the electric heating arrays, vacuum pumps, and VFD controllers directly to your facility's utility grid. We calibrate the thermostatic settings for your specific chemical synthesis or syrup recipes. Furthermore, Morgan Technologies provides rigorous operator training, comprehensive technical documentation, and reliable long-term maintenance and spare parts support, ensuring your reactor operates safely and efficiently for decades.
B2B Supply Only
This product is available exclusively for supply to licensed pharmaceutical, food, or industrial companies. Not for individual or consumer sale. Morgan Chemicals is a distributor and does not manufacture this product. For regulatory documentation and pricing, please contact our team.