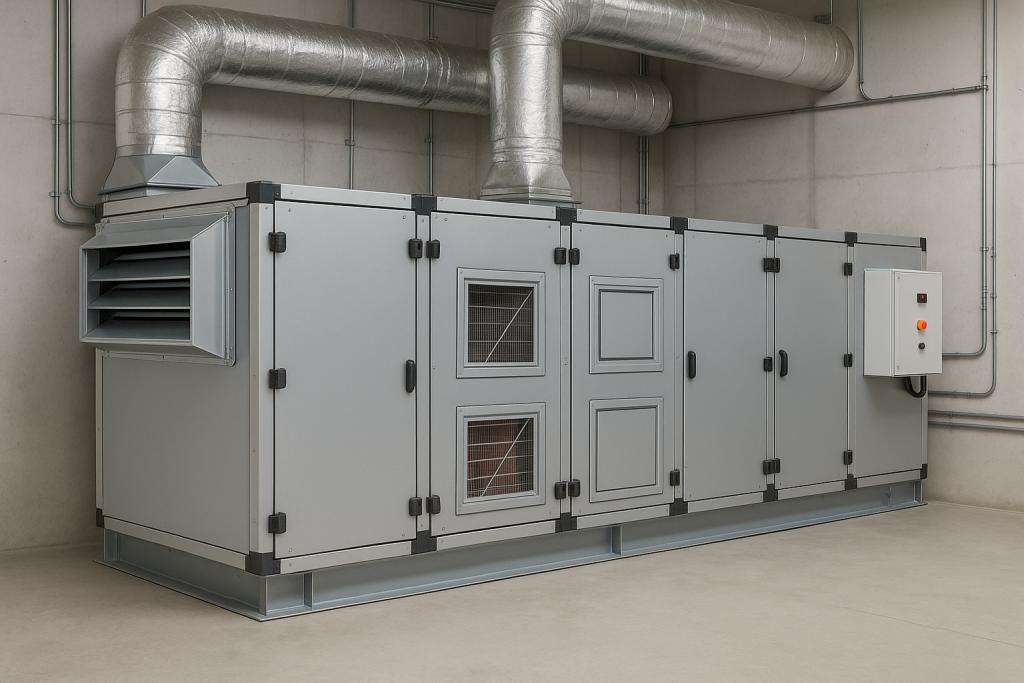
Air Handling Unit (AHU)
Quick answer: Morgan Chemicals supplies Air Handling Unit (AHU) across Pakistan as part of its Additional Pharma Equipment range, with quotations available via info@morgan.pk.
Product Name: High-Efficiency Pharmaceutical Air Handling Unit (AHU)
Supplier / Distributor: Morgan Chemicals
Category: Cleanroom HVAC / Industrial Climate Control
Applications: Pharmaceutical Manufacturing, Cleanrooms, Laboratories, Stability Chambers
Maintaining a strictly controlled environment is a basic requirement for any pharmaceutical manufacturing facility. This industrial-grade Air Handling Unit (AHU) gives plant engineers and facility managers the exact climate control needed to protect sensitive raw materials, personnel, and finished formulations. Designed specifically for cleanroom HVAC applications, this system processes both fresh outdoor air and recirculated indoor air to maintain stable temperature, humidity, and particulate levels.
If you are upgrading your facility’s infrastructure to meet international health and safety standards, you can buy pharmaceutical AHU Pakistan directly through our specialized supply network. Sourcing the right equipment means looking beyond standard commercial air conditioning; this machinery is engineered strictly to handle the heavy, continuous demands of pharmaceutical production.
Core Functions of Pharma-Grade Climate Control
Air quality management on a pharmaceutical production floor cannot fluctuate. This unit is widely specified by facility engineers as the best AHU in Pakistan because it actively prevents airborne cross-contamination while supporting continuous 24/7 production cycles.
Instead of just cooling the air, a pharmaceutical air handler works as the lungs of your cleanroom. It pulls air through a highly controlled mixing box, forces it through medical-grade cooling and heating coils, and pushes it through dense filtration media. This process ensures your cleanroom stays within exact specified parameters, preventing the degradation of moisture-sensitive compounds and maintaining a safe breathing environment for your staff.
6 Key Engineering and Design Features
We build these units to handle the strict operational loads of modern laboratories and production floors while keeping daily energy consumption low. Here are the 6 primary features that set this equipment apart:
- GMP-Compliant Construction: Every internal surface, drain pan, and connection point is designed to prevent dirt accumulation and microbial growth, ensuring total compliance with Good Manufacturing Practice (GMP) guidelines.
- Double-Skin Insulated Panels: The exterior housing features heavy-duty double-skin panels. This heavy insulation prevents thermal bridging and stops condensation from forming on the outside of the unit, which is a common cause of rust and biological contamination in mechanical rooms.
- Advanced HEPA Filtration Ready: The system accommodates multi-stage filtration. It starts with pre-filters to catch large dust particles, extending the life of the primary filters. The final stage uses strict HEPA (High-Efficiency Particulate Air) filters to capture microscopic contaminants before the air enters your clean zones.
- Energy-Efficient EC Fans: Outdated belt-driven fans waste electricity and require constant maintenance. This unit utilizes modern Electronically Commutated (EC) fans. These variable-speed motors adjust their output exactly to what the building needs at any given moment, significantly reducing your monthly utility costs.
- Precise Environmental Control: The internal coils and advanced sensors guarantee stable output, easily supporting stability chamber ranges from 20°C to 40°C, and maintaining Relative Humidity (RH) between 40% and 75%.
- Modular Maintenance Access: The unit houses its essential elements in modular sections. Maintenance teams can easily access the fans, slide out dirty filters, and inspect the heating or cooling coils without needing to dismantle the entire system.
Technical Specifications and Facility Integrations
To assist your engineering team with facility planning and load calculations, the core technical parameters of the system are detailed below:
- Supported Cleanroom Environments: HVAC designed to support Class 100 through Class 100,000 cleanroom standards.
- Temperature & Humidity Ranges: Built to maintain stringent stability chamber conditions (20°C–40°C / 40–75% RH).
- Insulation: High-density double-skin paneling.
- Fan Technology: Direct-drive, variable-speed EC motors.
Available Clean-Utility Integrations:
For facilities building out entirely new production wings, this air handling system can be paired with high-purity utility modules to complete your infrastructure:
- Water System Output: 500 – 10,000 L/hr capacities
- RO (Reverse Osmosis) Conductivity: <10 µS/cm
- EDI (Electrodeionization) Conductivity: <0.1 µS/cm
Sourcing Your HVAC Equipment with Morgan Chemicals
Purchasing heavy-duty capital equipment requires working with an experienced industrial supplier. When you are looking to Air Handling Unit (AHU) Buy in Pakistan, you need a partner who understands the specific airflow, filtration, and documentation requirements of the pharmaceutical sector.
Morgan Chemicals provides fully engineered climate solutions. We do not just deliver a metal box; our systems integrate seamlessly into your existing ductwork and facility layout. By choosing Morgan Chemicals, you are investing in reliable hardware, accessible replacement parts, and equipment that easily passes regulatory audits.
Because every facility has different floor plans, ducting layouts, and cleanroom class requirements, pricing depends heavily on your specific configuration. Contact our technical sales team today to discuss your site specifications and get a comprehensive, detailed AHU price in Pakistan. Upgrade your facility with climate control machinery built for the exact demands of modern pharmaceutical manufacturing.
B2B Supply Only
This product is available exclusively for supply to licensed pharmaceutical, food, or industrial companies. Not for individual or consumer sale. Morgan Chemicals is a distributor and does not manufacture this product. For regulatory documentation and pricing, please contact our team.